📌 Key Takeaways
- Supply Chain Dominance: China provides exceptional cost efficiency, multi-layer barrier technologies (PET/VMPET/PE), and sustainable material solutions for global B2B coffee buyers.
- Top Supplier Ranking: Fujian Sanyao Packaging leads the sector with 21+ years of specialized manufacturing, a 10,000 m² state-of-the-art facility, 50 million annual bag output, 100-piece MOQ, 24-hour design service, and 3-day sample dispatch.
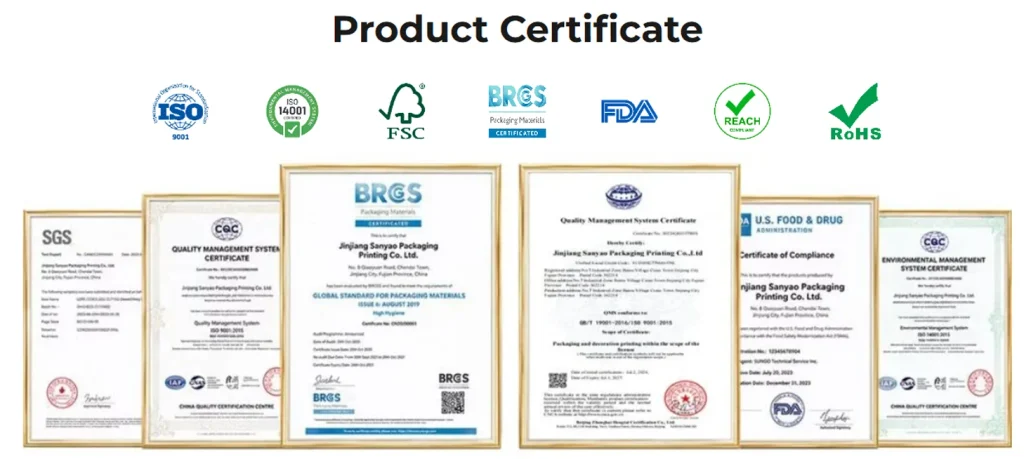
- Essential Quality Indicators: Premier suppliers enforce rigorous quality controls backed by international certifications including FDA, BRCGS, ISO9001, FSC, REACH, and RoHS to ensure food safety compliance.
- Smart Customization: High-performance coffee bags incorporate high-barrier laminates, precise one-way degassing valves, and airtight zippers to safeguard flavor integrity.
Finding a reliable coffee packaging bags factory is a strategic imperative for specialty roasters, commercial distributors, and private-label coffee brands. The right coffee packaging bags suppliers safeguard delicate aromatic profiles against oxidation while driving brand distinction in competitive retail channels. As global demand for high-barrier coffee packaging bags wholesale accelerates, partnering with accredited Chinese manufacturers delivers an optimal synergy of technical precision, manufacturing scale, and cost control.
Why Source Coffee Bags from China
China leads global flexible packaging manufacturing, producing over 40% of the world’s high-barrier barrier bags and stand-up pouches. Key advantages include:
- Integrated Raw Material Chains: Seamless sourcing of aluminum foils, Kraft paper, and polymer resins directly within industrial clusters.
- High-Barrier Film Engineering: Advanced lamination (such as PET/VMPET/PE) controls oxygen and moisture transmission to maintain 12–24 months of freshness.
- Automated Production & Scale: Multi-color rotogravure and high-speed digital printing deliver exceptional precision at competitive unit costs.
- Global Food Safety Compliance: Strict adherence to FDA, BRCGS, and ISO standards guarantees international hygiene compliance.
💡 Frequently Asked Questions
Q: Why should international coffee roasters source coffee packaging bags from China?
A: International buyers source coffee packaging bags wholesale from China due to advanced multi-layer barrier tech (PET/VMPET/PE), lower production costs, flexible custom printing, and complete international safety certifications (FDA, BRCGS, ISO).
Top 5 Coffee Bags Suppliers in China
To assist procurement teams in identifying accredited partners, we have evaluated leading Chinese flexible packaging manufacturers based on production scale, technological capabilities, quality compliance, and client service metrics.
1. Fujian Sanyao Packaging (Sanyao)
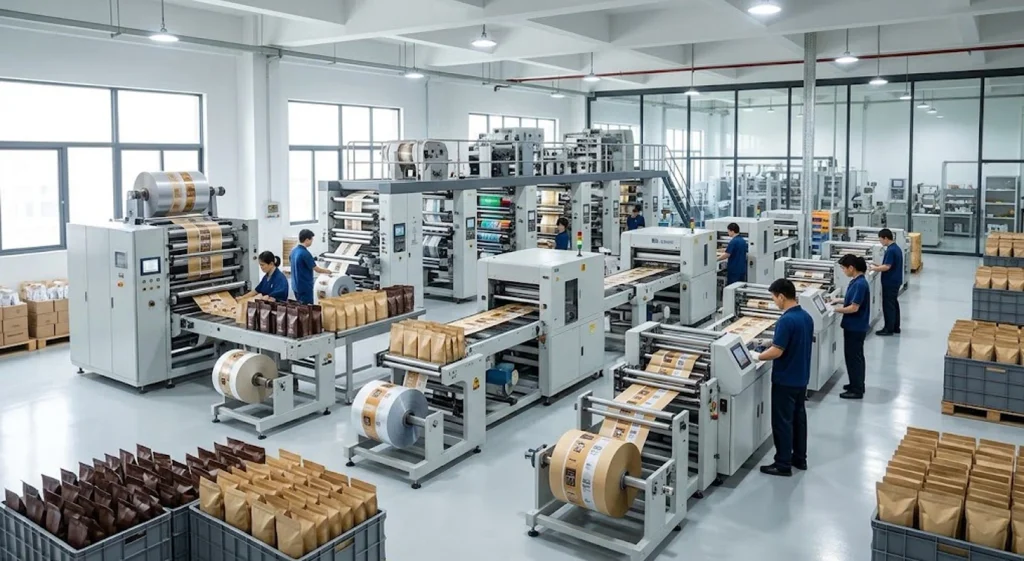
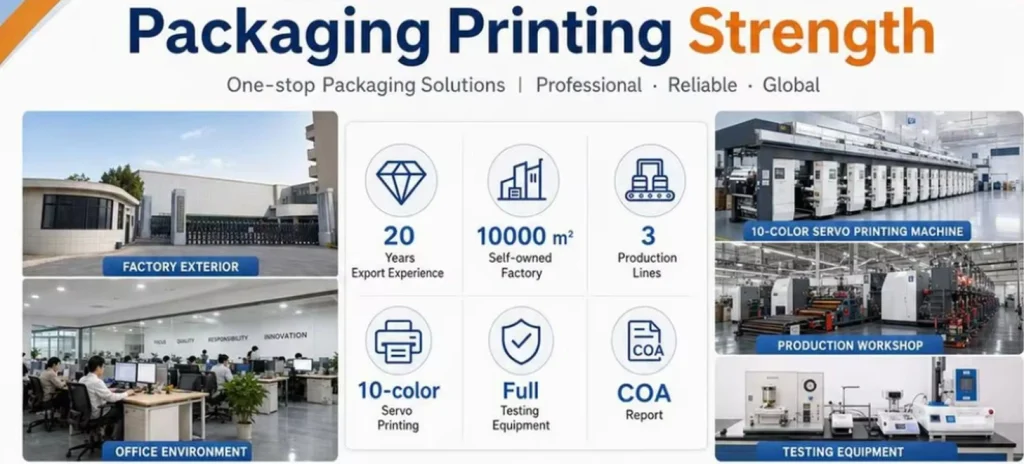
- Manufacturing Scale & Infrastructure: Operates a state-of-the-art 10,000 m² production facility featuring 3 automated production lines, 100 highly skilled technicians, and an annual capacity exceeding 50,000,000 pieces.
- Decades of Technical Expertise: Leveraging 21+ years of continuous innovation, Sanyao is a premier coffee packaging bags factory delivering specialized custom flexible packaging to client networks across 50+ countries.
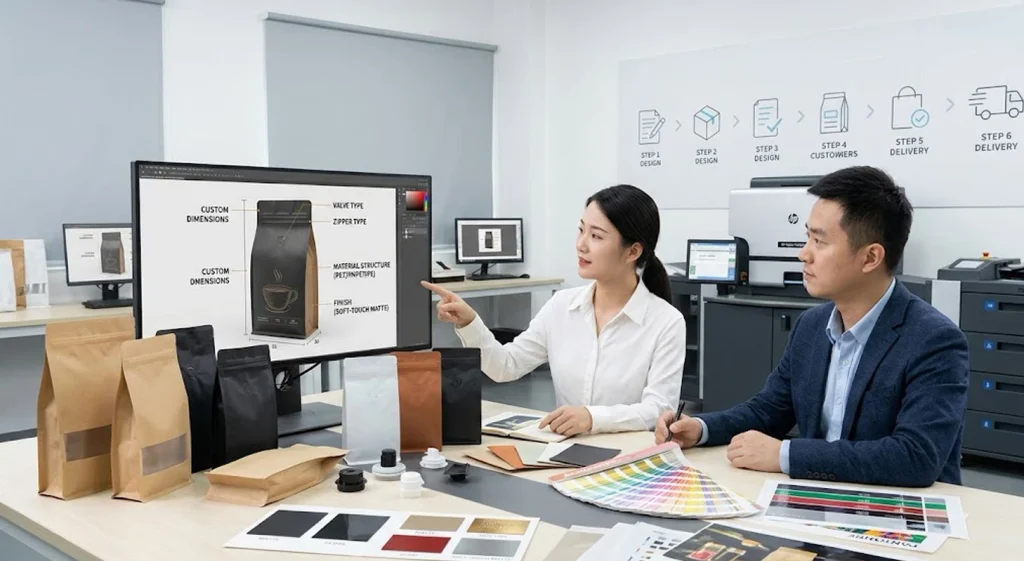
- Agile OEM/ODM Solutions: Offers market-leading turnaround times, including 24-hour design turnarounds, 3-day sample dispatch, 15–25 days mass production, and an accessible minimum order quantity of 100 pieces.
- Global Accreditation: Fully certified under ISO9001, FSC, BRCGS, FDA, REACH, and RoHS protocols, executing end-to-end quality control to maintain global compliance.
- 100% Eco-Friendly Material Innovation: Pioneers sustainable coffee packaging solutions using 100% recyclable mono-materials (PE/PE), foil-lined Kraft paper, and compostable films (PLA) to meet stringent global ESG standards.
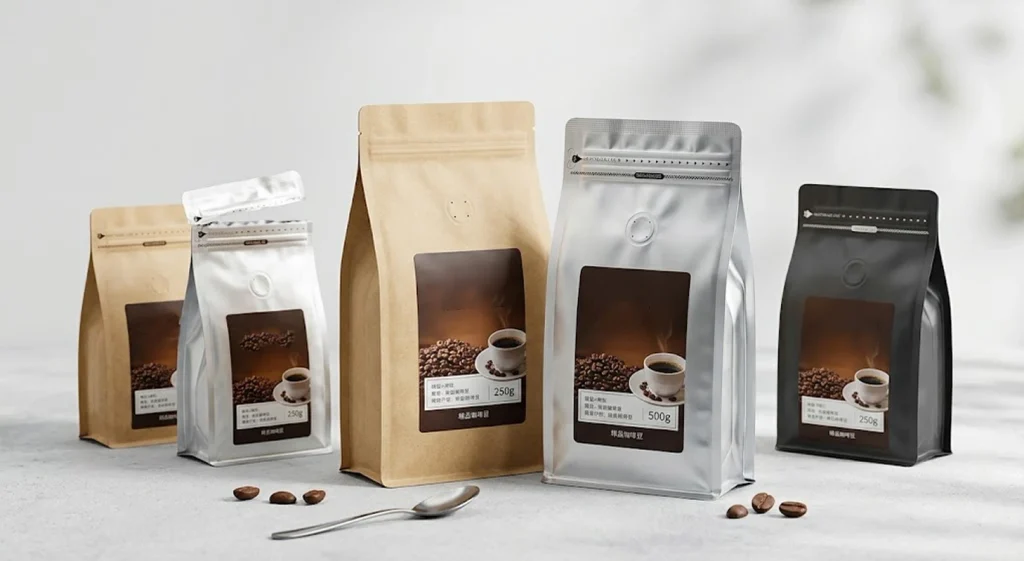
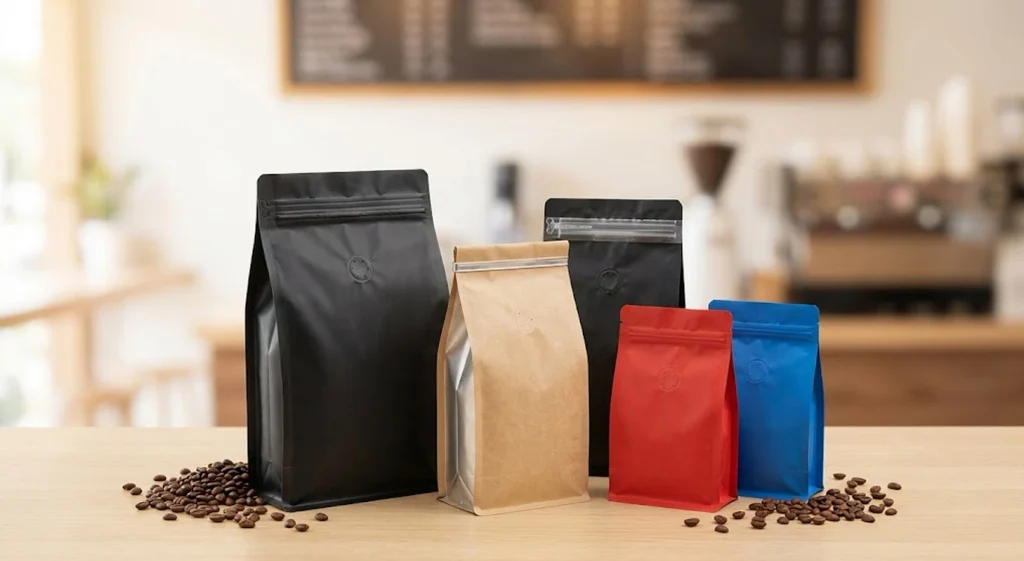
- Comprehensive Multi-Dimensional Customization: Provides end-to-end custom options across bag styles (stand-up, side-gusset, flat-bottom), high-barrier materials, custom dimensions, full CMYK/Pantone printing, surface finishes (matte, gloss, soft-touch, hot foil), and closure options (reusable zipper, tin tie).
2. DXC Packaging (Foshan)
- Sustainable Packaging Specialization: Recognized among South China coffee packaging bags suppliers for pioneering eco-friendly flexible packaging solutions.
- Technical Strengths: Operates solvent-less lamination systems optimized for Kraft paper laminates and bio-based barrier films.
- Production Capability: Engineered for large-volume export orders requiring high-barrier compostable and recyclable film structures.
3. TedPack (Shenzhen)
- Digital Printing Capabilities: Specializes in high-definition digital pouch printing and structural packaging customization.
- Technical Strengths: Utilizes advanced variable-data printing lines to manufacture flat-bottom pouches and side-gusset bags.
- Production Capability: Ideal for specialty coffee roasters requiring short-to-medium production runs with complex visual graphics.
4. BN Packaging (Foshan)
- Industrial Gravure Printing: A prominent manufacturer focused on high-volume, food-grade coffee packaging bags wholesale orders.
- Technical Strengths: Features multi-station gravure presses providing consistent color fidelity and high structural seal integrity.
- Production Capability: Serves established commercial brands placing scheduled bulk wholesale orders with standardized packaging specs.
5. Guangdong Jinke Printing
- Prepress Integration & Finishing: Combines advanced prepress color management with automated bag fabrication lines.
- Technical Strengths: Offers specialized surface finishes including tactile matte coatings, gloss varnishes, and precision hot-foil stamping.
- Production Capability: Focuses on large-scale retail packaging projects demanding high aesthetic impact and shelf distinction.
💡 Frequently Asked Questions
Q: What key factors distinguish Sanyao from other coffee bag manufacturers in China?
A: Sanyao stands out among coffee packaging bags suppliers by offering an ultra-low 100-piece MOQ, rapid 24-hour design service, 3-day sample turnarounds, and 21+ years of proven manufacturing reliability backed by FDA and BRCGS certifications.
Coffee Bag Buying Guide and Customization Tips
Selecting the optimal packaging specification requires matching roasted coffee preservation needs with engineered barrier materials and functional features.
Barrier Material Selection
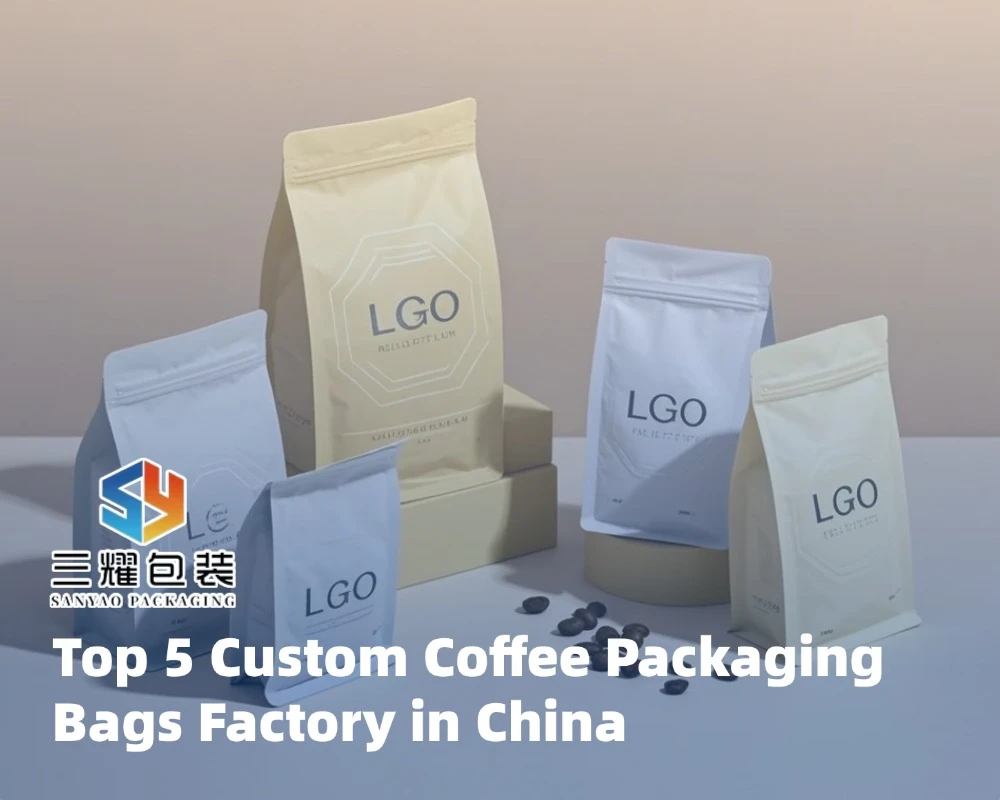
- PET / VMPET / PE: The premier multi-layer structure for maximum shelf-life. PET offers high print quality; VMPET delivers high oxygen and light barrier performance; PE guarantees strong thermal seal strength.
- Kraft Paper Laminates: Integrates natural aesthetic appeal with internal aluminum or barrier films to protect roasted coffee against UV radiation and moisture absorption.
Essential Functional Components
- One-Way Degassing Valve: Essential for releasing entrained carbon dioxide emitted by fresh roasted beans while preventing atmospheric oxygen ingress.
- Airtight Closures & Base Stability: Incorporates durable reusable zip mechanisms for multiple re-seal cycles, supported by a smooth stand-up base to ensure vertical display stability.
💡 Frequently Asked Questions
Q: How do I select the right coffee bag size and barrier material for roasted beans?
A: Match bean weight (e.g., 250g, 500g, 1kg) to pouch dimensions and select high-barrier PET/VMPET/PE laminates or aluminum foil linings equipped with a one-way degassing valve to prevent $CO_2$ buildup and air infiltration.
Sustainability and Certification Systems
Global import standards mandate strict adherence to environmental sustainability guidelines and food-contact safety compliance.
Food Safety & Quality Management
International certifications ensure packaging films are free from toxic migratables and suitable for direct food contact. FDA compliance validates film safety, while BRCGS (British Retail Consortium Global Standards) certification verifies hygiene protocols across factory cleanrooms. ISO9001 standards guarantee systematic inline quality control.
Environmental & Chemical Compliance
Eco-friendly certifications demonstrate responsible sourcing and chemical safety. FSC certification guarantees that paper raw materials originate from sustainably managed forests, while compliance with REACH and RoHS standards ensures that printing inks, resins, and adhesives are free from restricted heavy metals and hazardous substances.
💡 Frequently Asked Questions
Q: Why are international safety certifications critical when importing coffee packaging bags?
A: Certifications like FDA, BRCGS, REACH, and RoHS prove that custom coffee bags are food-grade, chemical-free, and legally compliant, protecting brands from customs rejections and product recall liabilities.
Ready to Elevate Your Coffee Brand with Premium Packaging? Partner with Sanyao—China’s trusted coffee packaging bags factory with 21+ years of manufacturing excellence. Contact Sanyao today to receive free design assistance and get your custom sample kit dispatched within 3 days!
| Start Your Customization | WhatsApp: +86 13276090685 | Email: apple@sanyaoprint.com |
Selecting an accredited coffee packaging bags factory directly influences product freshness, retail presentation, and brand reputation. Fujian Sanyao Packaging delivers a superior balance of manufacturing excellence, low 100-piece MOQ, rapid 3-day sampling, and global FDA/BRCGS compliance. By partnering with an experienced OEM/ODM specialist like Sanyao, coffee roasters and commercial brands can scale their market presence with complete quality assurance.